As presented at ARC Industry Forum · Speaking at ICC 2026
Underground Mining Solutions: Specialized Automation Solutions
Block Lighting Controls

This packaged system is designed to control single-lane traffic on underground ramps, featuring directional vehicle detection, pedestrian warning, and local and remote display options for effective notification. Built on Opto 22 Groov RIO edge controllers, it shows operators whether a ramp section is occupied and in which direction, preventing head-on encounters on blind grades and holding traffic clear when pedestrians are present. Each level is a complete standalone controller that grows the system one heading at a time, integrating seamlessly with our comprehensive underground automation solutions. An optional Groov EPIC surface controller adds ramp-wide visibility and event history.
Underground Pumping Control Solutions

Building on our Mud Level Detection solution, we can design, build, and install an underground pumping control solution tailored for local control, remote control, and monitoring of your water management system in underground mining applications. Our unique approach minimizes physical I/O, thereby reducing costs and panel size requirements, while enhancing insights into equipment health. Whether you need single or multi-pump systems, local HMI, cascading control between levels, or local/remote SCADA accessibility, we have you covered. Our systems include options for soft start and VFDs, alongside built-in advanced diagnostics for instruments and motor control devices. Additionally, we offer sump mud level detection, plugged and broken pipe detection, as well as sump and tank mud level diagnostics, ensuring robust performance and safety even with automated stench release systems.
Mining Shotcrete, Backfill, Mix Pit Solution

Our team of skilled technicians and programmers has years of experience in designing, specifying, and installing automation equipment and programs tailored for mining applications, including automated stench release systems and sump mud level detection for shotcrete and backfill plant retrofit or upgrade applications. OEM systems often fall short, providing only the bare minimum for efficient plant operation. We pride ourselves on being PLC system agnostic, with standard default options that include Rockwell or Opto22. Our extensive knowledge around instruments that just plain work for these demanding applications enables us to support you in making informed decisions upfront, ultimately minimizing maintenance costs and plant downtime in the long run. Additionally, our underground pumping control solutions and optional wireless silo telemetry add-ons are designed to enhance operational efficiency.
Auxiliary Vent Fan Controls

Do you have auxiliary ventilation fans underground? Do you monitor and control them remotely? If not, would it be beneficial to have remote control capabilities? Our automated stench release systems, combined with gas and airflow monitoring, enhance your auxiliary fan control solution and enable you to decrease post-blast clearance times. We can control up to 5 fans per panel location in our standard-sized solution, and additionally provide you with fan electrical monitoring data. If you need help modernizing the way you control your ventilation equipment underground, we are ready to assist you in achieving those goals.
Automated Stench Release Systems

For over 20 years, we have specialized in designing automated stench release systems for underground mines. As technology has advanced, so have our innovative designs. We proudly offer the most effective stench release system on the market, featuring modular components for easy local or off-site maintenance, along with built-in redundancy. Our systems include stench neutralization and line purge options, ensuring safety with a Class V valve shutoff for leak-free peace of mind. Additionally, we provide built-in local and remote controlled release methods via pushbuttons, HMI, and PLC connections. Our solutions also feature additional I/O capabilities for monitoring sump mud levels or controlling access gates as needed. If you've ever been tasked with maintaining a stench system in a mine, our automated solution will surpass your expectations for ease of use and long-term maintenance. Our systems ship ready to install at your location, with Modbus-TCP/IP or OPC UA communications connections available for remote SCADA integration.
Silo Automation and Telemetry Packages

Now featuring DuraPinch QTP valves with pneumatic or electric actuation and fail open or close options, our silo control and telemetry solution provides local silo level and alarm displays for operators, remote beacons for loader drivers, and automated fail-closed control of filling pinch valves, baghouses, and bin vibrators. Our added telemetry also provides remote access to silo and guppy levels for bulk commodities dispatching. Are you running out of cement without notice? Do you face issues with silo overfilling? Do you need to ensure your baghouse filter system operates as needed? If any of these scenarios describe your process, we can assist with our packaged solutions. Need to integrate historian data from the silos into your SCADA system? We can help with that too!
Portal Access Gates

Commercial gate controllers often struggle with the demanding conditions of a mining environment. To address this, we've developed a networkable and PLC controllable system that integrates seamlessly with your SCADA for both local and remote gate control. Our actuation equipment is specifically designed for mining applications, requiring only a 120VAC power connection with no air needed. The system features quick releasable, counterbalanced gate arms for emergency access and pairs perfectly with our automated stench release systems, providing a complete portal access solution. For areas requiring non-vertical entry, we offer additional options for underground horizontal gates. Replacement gate arms are easily sourced to ensure maintenance is straightforward. The system is shipped in sections to facilitate installation, considering the weight of the final package. Two model heights are available: one for free-standing use and one designed for mounting on a concrete 'Lego' or 'jersey' barrier. The gate arm length is field adjustable, accommodating lengths from 5' to 20', with 12'-15' lengths being the most common. We ship gate arms in shorter sections to save on freight costs. Furthermore, our solutions can be integrated with blast clearance and personnel safety in mind, enhancing the overall functionality of your operations.
Automated Pinch Valves
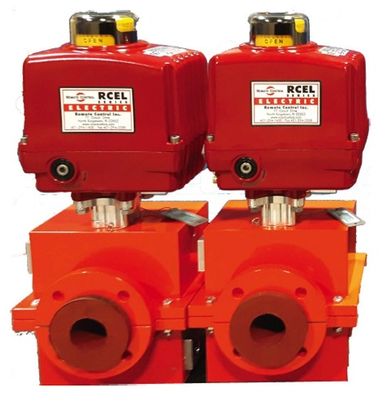
DuraPinch Series QTP quarter-turn pinch valves are designed to control abrasive slurries through a full-bore elastomer sleeve, with no metal components in the flow path to wear, seize, or pack off. The patented rotary design closes through mechanical lever arms rather than direct linear thrust, so actuator size and cost scale far better on large lines, where closing force otherwise rises exponentially with diameter. Suited to slurry, backfill, dewatering, and reagent service, these valves integrate seamlessly with our comprehensive underground pumping control solutions — sized, actuated, and commissioned as part of a controlled system rather than supplied as loose components.
Maestro Digital Mine
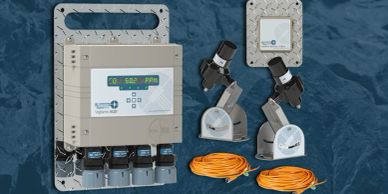
Maestro Digital Mine builds the ventilation monitoring and network hardware that underground automation depends on — Vigilante AQS™ V2 and Zephyr AQS™ air quality and quantity stations, MaestroFlex™ automated regulators, and the Plexus PowerNet™ gigabit network that carries power and data over standard coaxial cable. Together they make Ventilation on Demand practical, measuring airflow and gas where it matters, adjusting regulators to match equipment activity, and shortening blast clearance times. We integrate Maestro devices into site control and reporting, so ventilation data arrives in the same system as your pumping, dewatering, and traffic control.
Ultimo Density Measurement

The safe, low cost of ownership solution for slurry density measurement.
A Market-proven, in-line, non-invasive device for measuring all types of slurries in the most challenging situations.
PS Automation - Electric Actuation
PS Automation - Electric Actuation
ELECTRIC VALVE ACTUATION · MADE IN GERMANY — Precision electric quarter-turn and linear valve actuators, engineered and manufactured
in Germany since 1989.